
Why Complex Component Designs Need a Smarter Machining Strategy

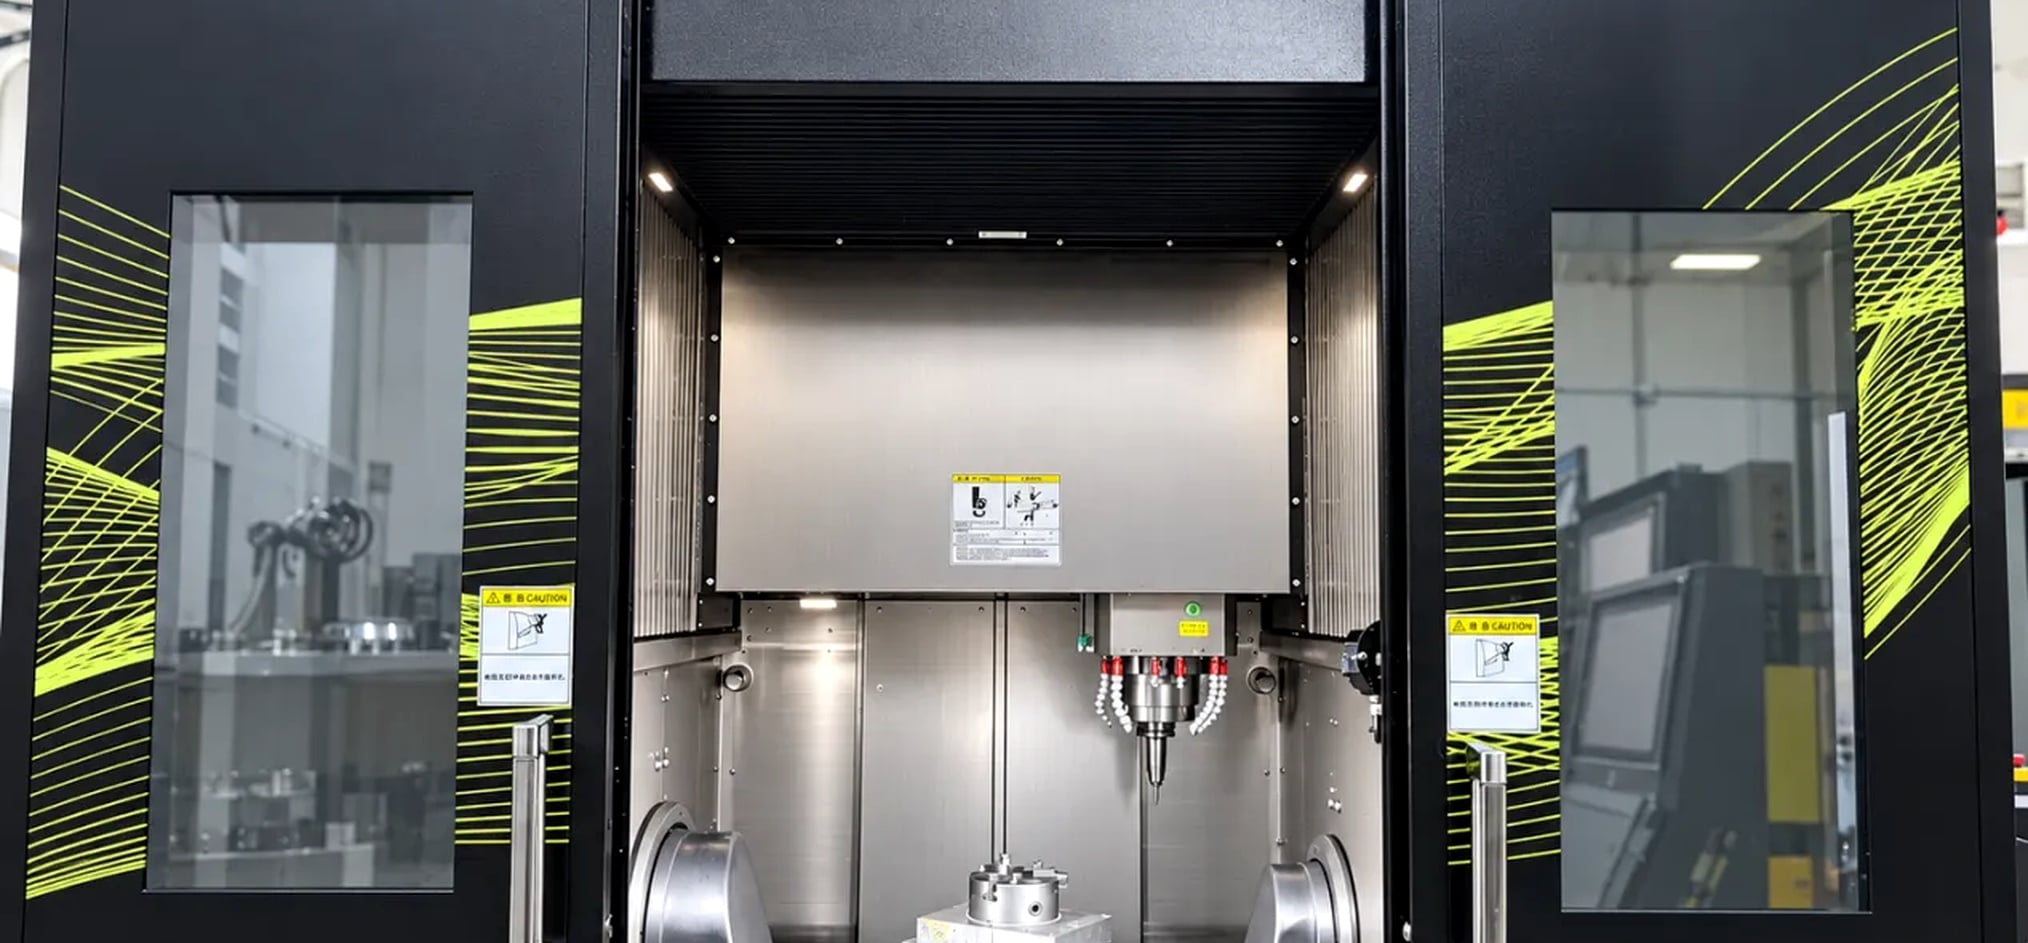
Manufacturing components with deep cavities, angled holes, undercuts, and complex surfaces presents challenges that conventional machining methods cannot always address efficiently. Multiple setups can increase alignment errors, production time, and manufacturing costs.
5-axis CNC machining offers a practical solution by providing greater tool accessibility, reducing workpiece repositioning, and supporting more efficient machining strategies. However, achieving reliable results requires careful planning of cutting tools, workholding, machining sequences, and quality control.
Understanding the Challenges of Complex Geometries
A component may look straightforward in a CAD model, but manufacturing it can reveal significant difficulties. Deep pockets, compound angles, thin walls, and overlapping surfaces often require cutting tools to approach the workpiece from different directions.
Conventional 3-axis machines can produce highly accurate components, but their limited tool orientation may require additional fixtures or multiple setups for complex geometries.
These difficulties become particularly important when several machined features must maintain precise positional relationships.
For example, an aerospace housing may contain bearing interfaces, angled mounting holes, and internal cavities that must align during assembly. Repositioning the workpiece between operations introduces additional variables, including locating errors and clamping-induced deformation.
An effective machining strategy must therefore consider the entire production sequence rather than treating each feature as an independent operation.
Reducing Setup Changes Without Sacrificing Accuracy
One important advantage of 5-axis CNC machining is its ability to approach multiple surfaces while keeping the workpiece secured in the same fixture.
By combining three linear axes with two rotational axes, the machine can position the cutting tool relative to the workpiece at different angles.
This flexibility can reduce the need for manual repositioning and additional workholding fixtures.
Fewer setups offer several potential benefits:
- Reduced opportunities for locating and alignment errors.
- Better consistency between features machined in the same setup.
- Less manual handling and intermediate fixture preparation.
- Improved accessibility to angled and multi-sided geometries.
However, fewer setups do not automatically guarantee tighter tolerances.
Machine calibration, fixture rigidity, thermal stability, cutting forces, and programming accuracy still influence dimensional results.
The objective is not simply to eliminate setups, but to select a manufacturing process that maintains accuracy while minimizing unnecessary operations.
Choosing Between Simultaneous and Indexed 5-Axis Machining
Not every complex component requires continuous movement of all five axes.
Two commonly used approaches are indexed 3+2 machining and simultaneous 5-axis machining.
Indexed 3+2 machining positions the cutting tool or workpiece at a selected orientation before performing conventional three-axis cutting.
It is particularly suitable for angled holes, flat surfaces, and features located on different sides of a component.
Because the rotational axes remain stationary during cutting, this approach can provide stable machining conditions and relatively straightforward programming.
Simultaneous 5-axis machining allows the linear and rotational axes to move together throughout the cutting operation.
This capability is especially valuable for complex curved surfaces, certain undercuts, and geometries that require continuously changing tool orientations.
However, simultaneous machining generally demands more sophisticated programming, machine simulation, and movement control.
Experienced manufacturers often combine both methods within the same component, using indexed machining wherever practical and simultaneous movement only where geometry requires it.
Why Tool Accessibility Matters in Precision Manufacturing
Tool accessibility is one of the most important considerations when planning complex CNC operations.
Deep cavities and narrow internal spaces often restrict the cutting tool’s approach angle. Conventional machining may require long tools to reach critical surfaces, increasing the risk of vibration, deflection, and poor surface finish.
Five-axis positioning can help overcome some of these limitations by allowing the cutting tool to approach a feature from a more favorable direction.
In suitable applications, this makes it possible to reduce tool overhang, improve cutting stability, and minimize interference with surrounding geometry.
However, additional rotational axes do not make every feature accessible.
Some internal undercuts still require specialized cutting tools, carefully selected holders, or modified machining sequences.
The most effective solution depends on the relationship between workpiece geometry, cutting tool dimensions, machine movement limits, and available fixture space.
How CAM Simulation Helps Prevent Machining Errors
Advanced machining capability depends on more than the machine itself. Computer-aided manufacturing (CAM) software plays an important role in converting complex CAD geometry into practical machining operations.
For demanding five-axis components, engineers use CAM software to plan toolpaths, evaluate cutting tool orientation, and verify machining movements before production.
Machine simulation can help identify several potential problems.
Tool and Holder Collisions
A cutting edge may reach a feature while the tool holder interferes with nearby cavity walls. Simulation allows programmers to evaluate clearance and adjust tool orientation or tooling configurations.
Rotary-Axis Interference
Complex five-axis movements can bring fixtures, workpieces, and machine components into close proximity. Machine-aware simulation helps identify potential interference before executing the program.
Inefficient Toolpaths
Poorly planned cutting movements may introduce unnecessary travel or unsuitable machining conditions. Toolpath optimization helps programmers improve the cutting sequence and reduce avoidable movements.
Nevertheless, simulation is not a substitute for proper machine setup or physical verification.
Accurate machine models, reliable postprocessors, appropriate workholding, and experienced operators remain essential for translating digital instructions into successful machining results.
Real-World Example: Machining a Complex Aluminum Housing
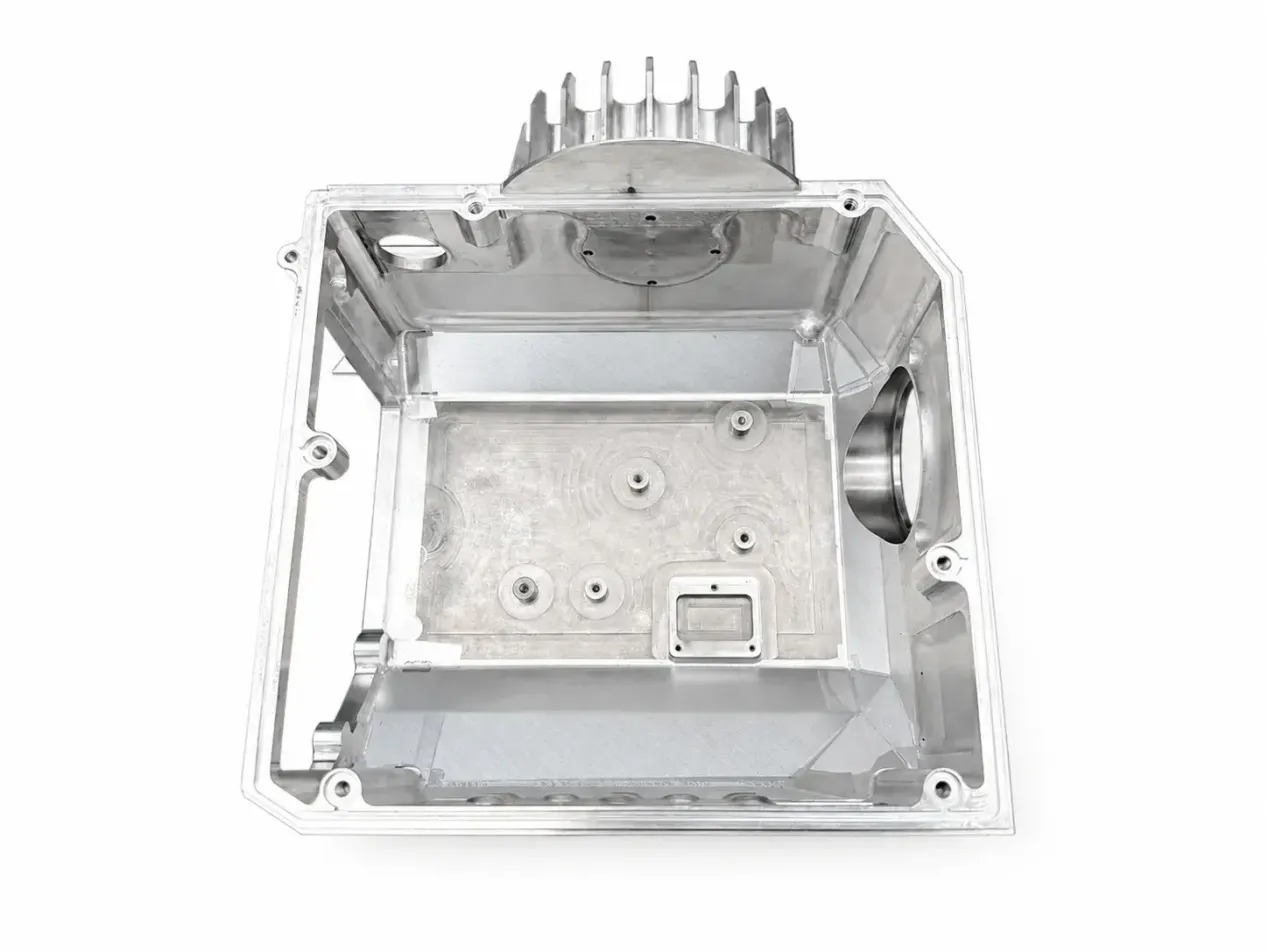
The practical value of combining five-axis machining with advanced process planning can be seen in an aerospace housing manufactured from 7075 aluminum alloy.
The component contained deep cavities, internal undercuts, thin walls, and complex multi-sided features.
These characteristics created several manufacturing challenges.
Restricted cavity access prevented standard ER tool holders from reaching certain undercuts, while extended tool overhangs increased the potential for vibration and cutting tool deflection.
According to a documented manufacturing case from YUANYI Precision Manufacturing, the engineering team used hyperMILL to perform a full-scale machining simulation before production.
The simulation helped verify toolpaths, tool-holder clearance, rotary-axis movements, and fixture positioning.
To access the restricted features, the team selected a shrink-fit tool holder and a small-diameter lollipop cutter.
The machining strategy combined indexed 3+2 operations for accessible surfaces with simultaneous 5-axis toolpaths for more demanding features.
Additional support stock was retained during roughing to help minimize thin-wall deformation and machining vibration.
According to the manufacturer’s project documentation, the complex undercuts were completed without reported tool interference or collisions, and the finished component achieved a surface roughness of approximately Ra 0.4 μm.
This example demonstrates how effective https://www.yycncmachining.com/5-axis-cnc-machining-services/ 5 Axis CNC Machining Services rely on integrated engineering decisions involving CAM programming, specialized tooling, workholding stability, and machining strategy.
It also highlights why selecting an appropriate manufacturing process requires more than comparing machine specifications.
Quality Control Begins Before Production
Dimensional accuracy depends on decisions made throughout the manufacturing process, not only during final inspection.
Before machining begins, engineers should review critical dimensions, datum references, geometric tolerances, and inspection accessibility.
These requirements influence fixture design, cutting sequences, and the selection of appropriate measurement methods.
For complex multi-sided components, maintaining the relationship between critical features can be as important as meeting individual dimensional tolerances.
During manufacturing, in-process inspections can help identify dimensional deviations before additional machining operations are completed.
Coordinate measuring machines, precision gauges, and documented inspection procedures provide further verification after production.
A suitable quality-control plan should prioritize features that affect assembly, fit, and component function rather than treating every measurement as equally critical.
Making Advanced Machining Economically Practical
Five-axis machining generally requires more advanced equipment, programming capabilities, and operator expertise than conventional three-axis machining.
Consequently, it is not automatically the most economical option for every component.
Simple parts with accessible features may be manufactured more efficiently using conventional machining processes.
For complex components, however, multi-axis machining can reduce some of the additional fixtures, repositioning operations, and manual handling required by traditional methods.
These improvements may offset higher machine-hour costs, particularly when components have demanding geometric relationships or difficult-to-access features.
Manufacturers should evaluate total production costs, including programming, setup time, tooling, machining operations, inspection, and potential rework.
The appropriate machining strategy depends on component complexity, tolerance requirements, material behavior, and production volume.
In many cases, combining conventional machining with selected five-axis operations provides a more practical solution than applying the most advanced process to every feature.
Conclusion
Successful manufacturing of complex components requires more than advanced CNC equipment. Part geometry, tool accessibility, machining strategy, CAM simulation, workholding, and quality control must be considered together.
Five-axis CNC machining offers valuable flexibility for producing deep cavities, curved surfaces, angled features, and multi-sided components while potentially reducing setup requirements.
For engineers developing aerospace, robotics, and other precision mechanical components, the most effective approach is to evaluate the complete manufacturing process rather than individual machining operations.
Manufacturers such as YUANYI Precision Manufacturing demonstrate how practical engineering experience, multi-axis machining technology, and digital process planning can be combined to address challenging component designs.




Comment