
High-Protein Puff Snacks: What to Test Before Commercial Scale-Up

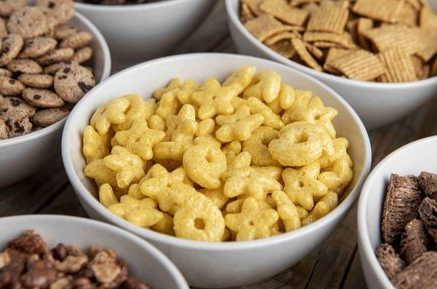
High-Protein Puff Snacks: What to Test Before Commercial Scale-Up
A high-protein puff can leave a pilot extruder crisp and well expanded, then turn dense, hard, or uneven on a commercial line. The change is not minor. In a 2025 Food Science & Nutrition trial using lentil flour and corn grits, changes in lentil flour content, feed moisture, and barrel temperature moved the expansion ratio from 3.55 to 1.55. Apparent density ranged from 0.43 to 2.63 g/cm³, while hardness rose from 86.72 N to 399.63 N. A formula that delivers more protein can therefore lose the structure that makes a puff enjoyable.
Commercial scale-up should not begin with a larger motor or a headline output figure. It should begin with a controlled test plan. Manufacturers need to define the finished product, lock the raw-material specifications, map the workable process window, and verify drying and line balance. Only then can a supplier select equipment around measurable production needs.
Why Can a Successful Pilot Formula Fail at Full Scale?
Extrusion combines conveying, mixing, cooking, pressure development, expansion, shaping, and cutting in one continuous process. Changing machine size alters more than kilograms per hour. Barrel fill, residence time, heat transfer, die pressure, and the balance between thermal and mechanical energy may all change. Copying pilot temperatures and screw speed is therefore not a complete scale-up recipe.
Two pea protein concentrates with the same declared protein percentage may differ in particle size, water absorption, fat, fiber, and previous heat treatment. Those differences can alter feeding, expansion, and color. The main variables fall into three connected groups: formulation, thermomechanical cooking, and die texturization. All three remain connected during scale-up.
Define the Saleable Product Before Testing the Process
“A crisp high-protein snack” is not a useful acceptance standard. Define its protein, density, shape, piece weight, moisture, and texture. Otherwise, each trial can appear successful for a different reason.
Use the approved bench or pilot sample as the reference, then attach measurable limits.
| Control point | What to define | Why it matters at scale |
| Protein target | Finished-product protein per 100 g and per serving | Determines the workable ingredient range and label position |
| Expansion and density | Expansion ratio, bulk density, and piece weight | Separates a light puff from a compact or inconsistent product |
| Shape | Diameter, length, wall thickness, and cut tolerance | Exposes die, cutter, and pressure variation |
| Texture | Instrumental hardness plus sensory crispness | Prevents a nutritionally acceptable but unpleasant product |
| Moisture control | Moisture and water activity after cooling | Affects crispness, seasoning, microbial risk, and shelf stability |
| Commercial output | Acceptable finished kilograms per hour | Prevents rejected pieces from being counted as capacity |
A dense protein crisp used in a nutrition bar has a different texture brief from a direct-expanded retail puff. Set limits around the intended eating experience, pack format, shelf life, and nutritional claim.
Test the Formula as a Processing System
Keep Enough Structure for Expansion
Starch normally supplies much of the expandable matrix in a puffed snack. Protein can strengthen nutrition, but it also competes for water and interrupts that matrix. As the protein fraction rises, gas cells may expand less or collapse sooner. The result can be smaller pores, higher density, and greater hardness.
Test a narrow series of protein-to-starch ratios. For each one, record expansion, density, motor load, die pressure where available, and texture after cooling. A slightly lower inclusion may produce a better snack while still meeting the planned claim.
Protein source matters too. Soy, pea, lentil, chickpea, rice, wheat, and dairy proteins do not behave identically. A blend selected for amino-acid profile or label appeal still needs an extrusion trial.
Control Particle Size, Fat, Fiber, and Water
Fine powders can feed differently from coarse cereal grits. Broad particle-size distribution may cause hopper segregation. Fiber absorbs water and can weaken expansion, while fat may reduce mechanical energy input by lubricating the mass.
Record particle-size range, moisture, fat, fiber, bulk density, and any heat treatment that may affect functionality. Retain approved-lot samples for comparison.
Test feed moisture as a range. Too little can create high load, poor cooking, or unstable flow. Too much can reduce die expansion and produce a soft, compact piece. Choose a setting that delivers repeatable quality without pushing the drive or temperature controls close to their limits.
Map the Process Window Before Selecting Production Equipment
Stabilize Feeding and Preconditioning
A fluctuating feeder creates a fluctuating product. Before changing barrel temperatures, check whether dry feed and liquid addition are steady. Powders that bridge or separate may require another hopper or agitation method.
Preconditioning can distribute water or steam before the screw. Record dry feed, added water, steam where used, conditioner conditions, and inlet material temperature.
Record Mechanical Load, Not Just Setpoints
Temperature setpoints do not describe the complete treatment received by the food. Record actual temperatures, screw speed, motor load, feed and liquid rates, die pressure when measured, cutter speed, and product output.
A trial that produces five attractive minutes between repeated surges is not ready for scale-up. Run to steady conditions and compare samples collected at intervals for color, dimensions, density, moisture, and texture.
Treat the Die and Cutter as Product Tools
Die design affects pressure, cell development, and shape. Cutter speed and blade condition affect length, torn edges, fines, and piece-weight consistency. Include both in the trial plan.
If several shapes are planned, test the highest-risk die. Each important SKU needs a defined configuration, changeover procedure, and expected output.
Do Not End the Trial at the Extruder Discharge
A puff can look crisp when warm and soften after seasoning or packing. Drying must remove moisture evenly without causing cracks or excessive browning. Cooling must prevent condensation. Oil and seasoning then change surface moisture and package behavior.
Measure moisture after extrusion, drying, cooling, and seasoning. Check samples again after 24 hours in the intended package. Shelf-life work should cover water activity, texture, flavor, seals, and target-market storage conditions.
The slowest section determines saleable line output. An extruder rated above the dryer, seasoning drum, cooler, or packing machine can create queues and quality drift. Capacity discussions should therefore use finished product after the complete process, not wet extrudate leaving the die.
Build a Trial That Can Become a Purchase Specification
Use the following sequence before requesting a commercial-line quotation:
Freeze the reference formula and identify every ingredient by supplier and grade.
Define measurable limits for protein, expansion, density, shape, texture, moisture, color, and finished yield.
Run a small trial matrix covering the most important formula and moisture variables.
Record feed, liquid, temperature, screw, load, die, cutter, drying, and output data for each acceptable sample.
Repeat the preferred condition with another raw-material lot and a longer stable run.
Convert the accepted result into factory-acceptance criteria and a commercial process brief.
This brief gives suppliers a basis for sizing the feeder, conditioner, extruder, die, cutter, dryer, cooler, seasoning system, and controls. It also makes quotations easier to compare.
At this stage, a small extrusion platform can reduce failed production trials. Arrow Machinery’s AHT36 experimental twin-screw extruder supports small-batch work with grains, starches, legumes, and mixed powders. Its modular barrel and screw arrangement allows formula and process comparisons before a production configuration is fixed.
For projects moving beyond trials, Arrow Machinery can connect the results with a complete puff snack processing line and its downstream stages. Buyers should request a written capacity basis, equipment list, utilities, layout, trial conditions, training scope, spare-parts list, and acceptance method.
The lowest-risk next step is simple: prepare a one-page trial brief with the target product, formula, ingredient specifications, required output, pack format, and acceptance limits. Send the same brief to each shortlisted supplier and ask how the pilot evidence will be translated into commercial equipment. Manufacturers ready to compare a laboratory trial with a full-line configuration can send this brief to Arrow Machinery for an initial project review.
FAQs
How much pilot material is needed before commercial scale-up?
It depends on feeder size, stabilization time, trial conditions, downstream testing, and samples required for sensory and shelf-life work. Calculate material by condition and include setup losses and repeat runs.
Can the same extruder produce standard corn puffs and high-protein puffs?
Possibly, but the formulas may require different screws, feeding methods, moisture addition, dies, temperatures, and drying conditions. Confirm change parts, cleaning work, and verified output for each product.
What capacity should appear in the purchase contract?
Use saleable finished output at agreed quality, not the highest instantaneous discharge rate. The capacity basis should identify the formula, raw-material condition, product dimensions, moisture, stable-run duration, accepted reject level, and downstream equipment included in the test.
Conclusion
Successful high-protein puff snacks depend on the relationship between formulation and equipment. Starch balance, ingredient functionality, water, mechanical energy, die behavior, drying, cooling, and packaging determine whether the snack remains light and crisp.
Scale-up becomes safer when the approved sample is converted into numbers, the process window is recorded, and the line is tested against saleable output. That evidence supports a stronger specification and fewer commissioning surprises.




Comment